Powder Coating and Surface Finishing Services
Coating is the last step, and the one the customer sees first. Pre-treatment, film thickness and cure control decide whether the finish still looks right after a year outdoors.
Finishing That Survives the Field
Most coating failures start before the powder goes on. Oil, laser dross or rust at the pre-treatment stage produce pinholes and poor adhesion that only appear after weathering. We degrease, rinse and pre-treat according to the substrate and the environment the part will work in, then apply and cure at controlled film thickness rather than by eye.
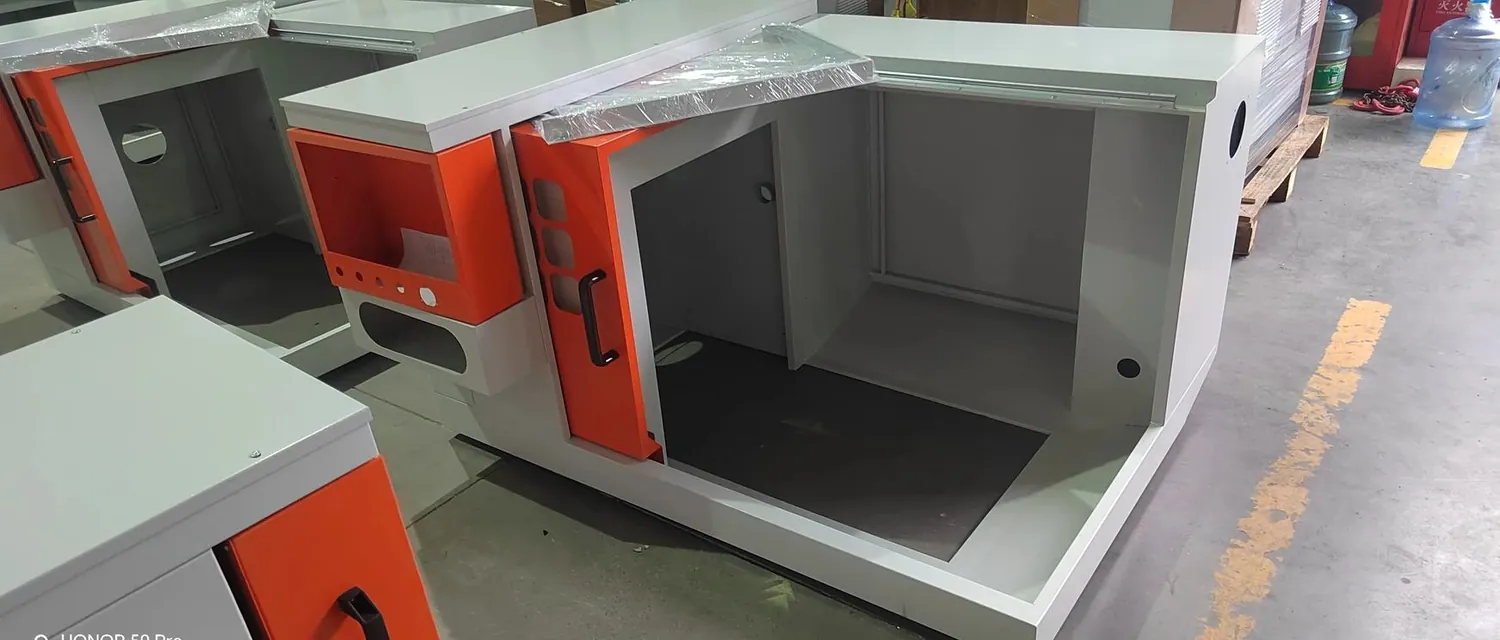
For outdoor equipment we also finish the edges and cut-outs properly: sharp laser edges are dressed so the coating does not pull back, masked threads and grounding points stay clean, and where a part needs a specific colour match for a brand or an installation, the RAL code is confirmed before the run rather than after.
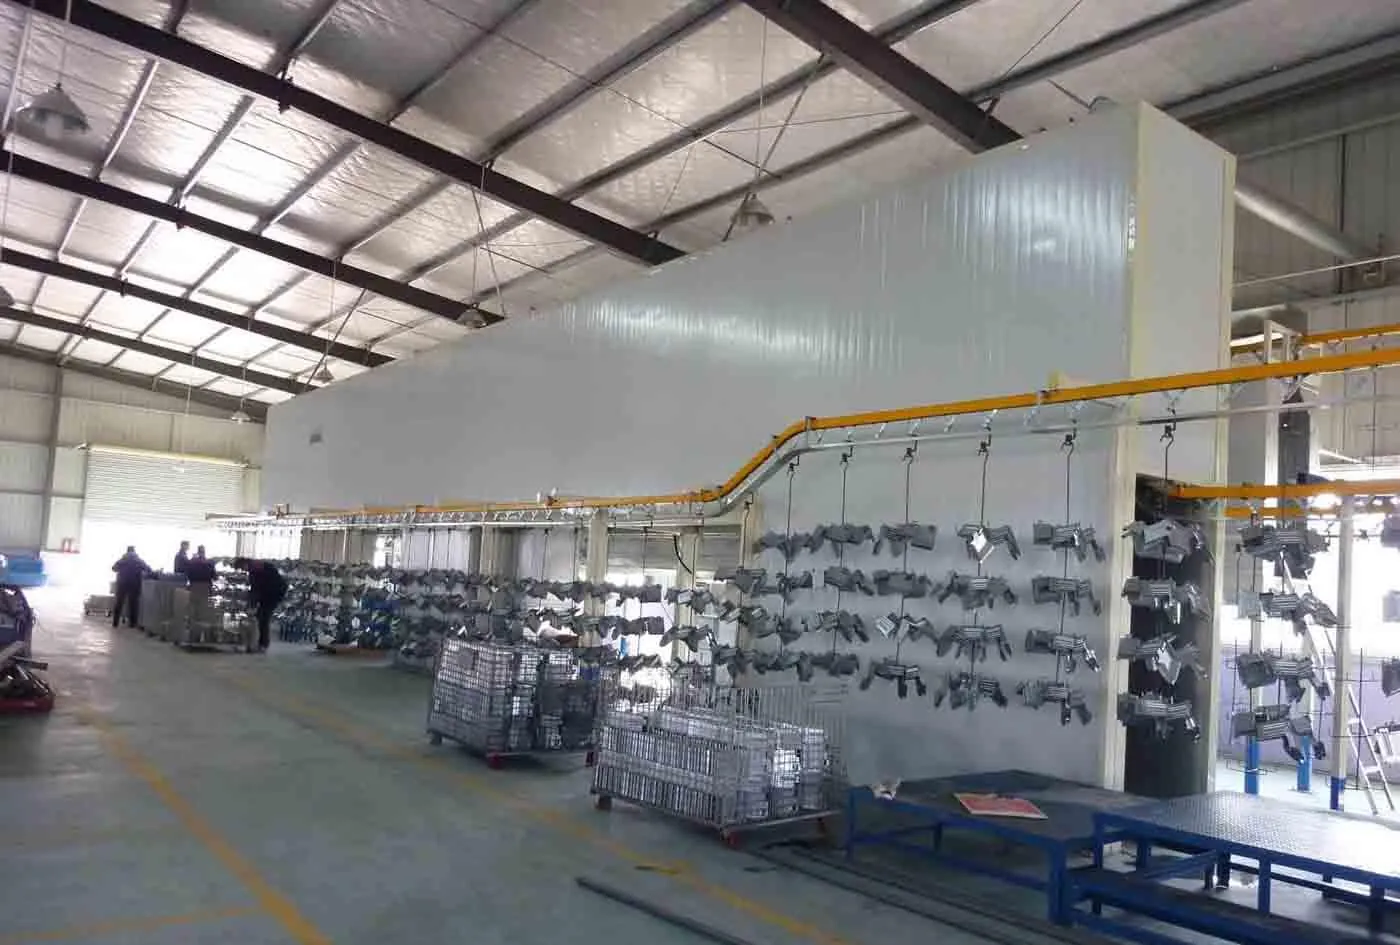
A Closer Look at This Capability
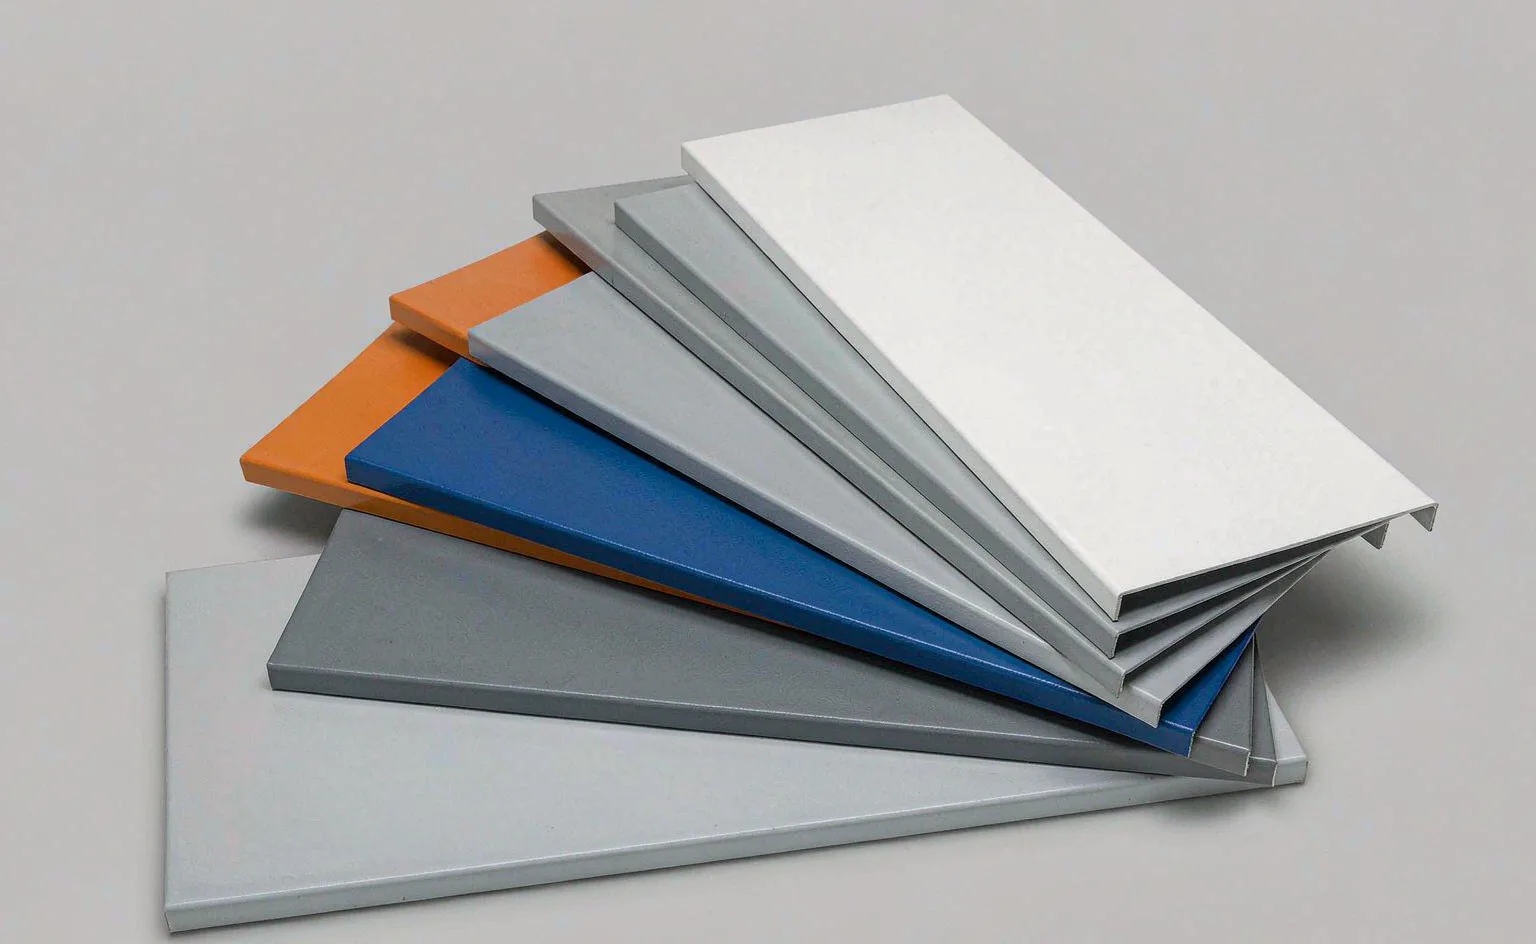
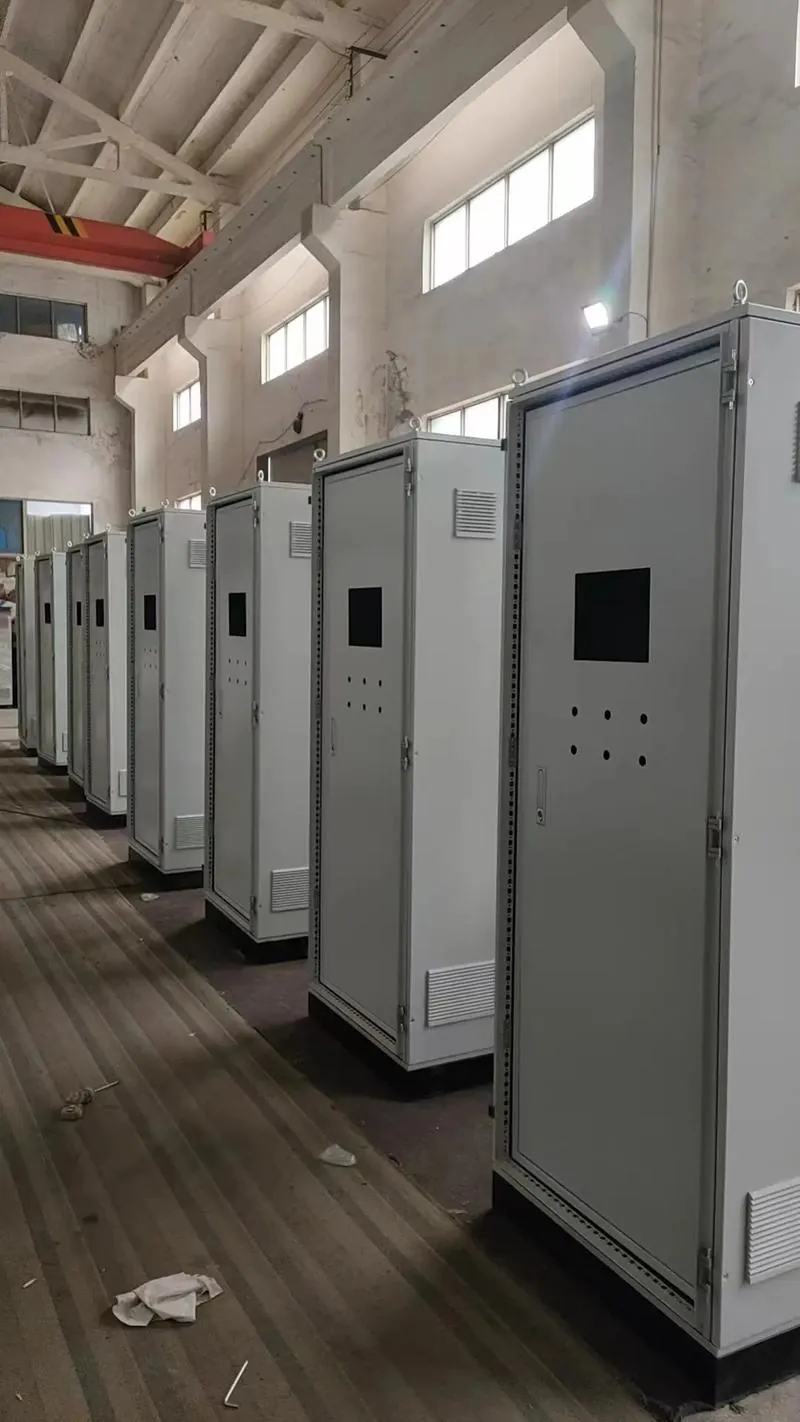
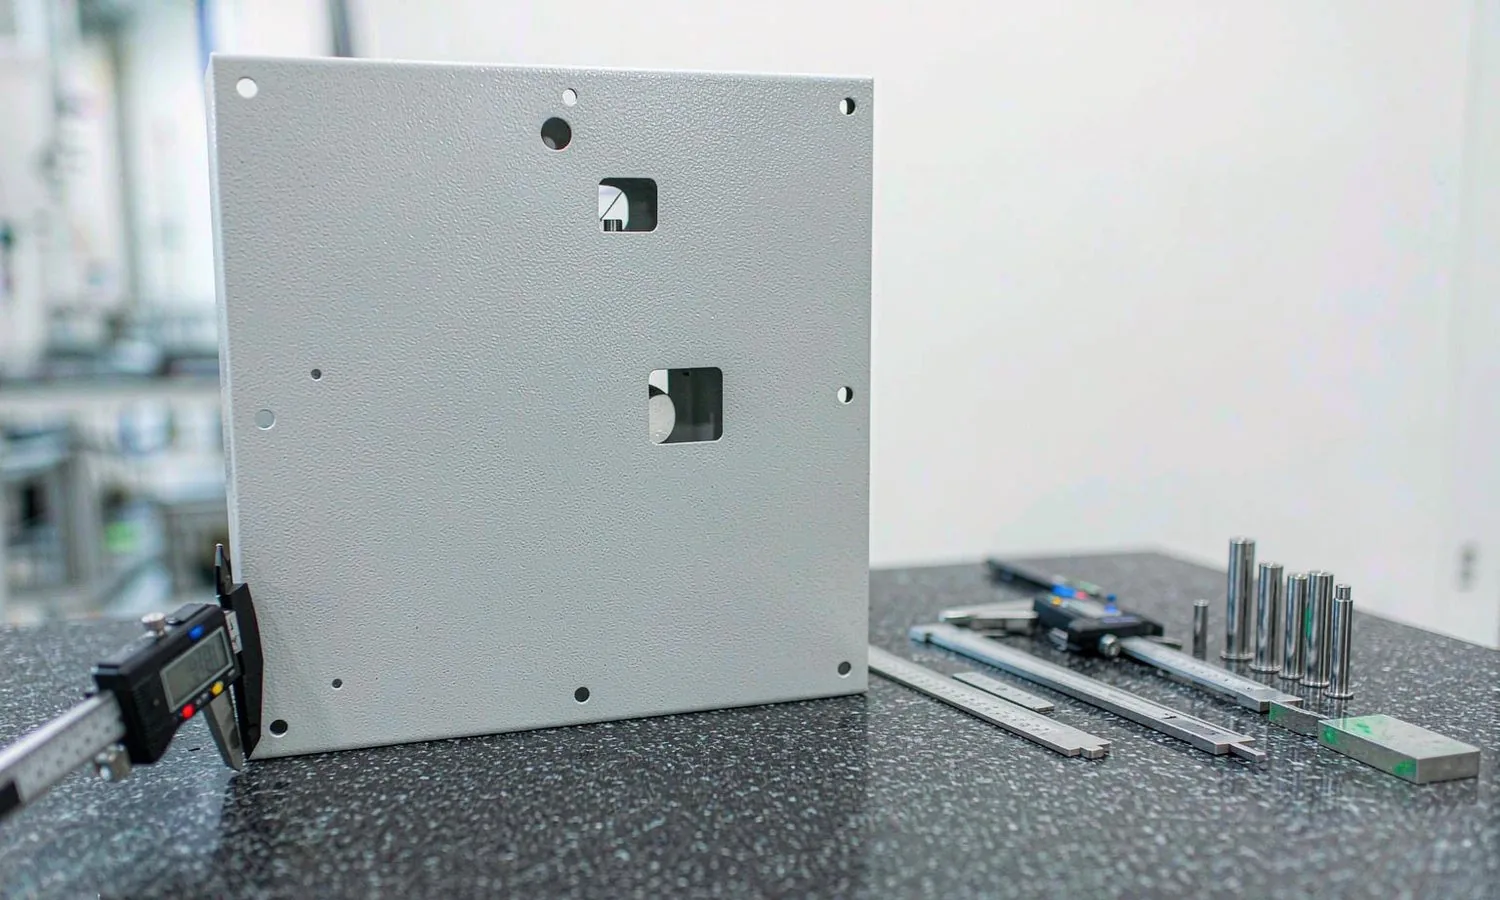
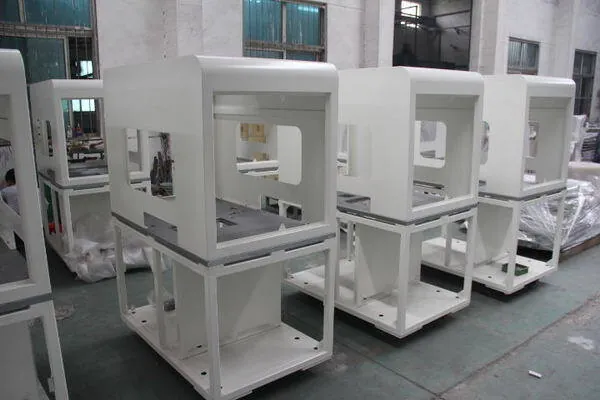
Representative photographs of the equipment, the process and the parts produced.

Specifications at a Glance
| Parameter | Typical Specification |
|---|---|
| Coating types | Powder coating in the full RAL range, plus texture, matte, satin and metallic effects on request |
| Substrates | Cold-rolled and galvanized steel; aluminium; stainless steel where a coloured finish is required |
| Pre-treatment | Degreasing and rinse stages selected by substrate and service environment, including phosphate and passivation |
| Film thickness | Typically 60-100 microns depending on the specification and the service environment |
| Cure control | Time and temperature controlled per powder system rather than by visual appearance |
| Corrosion testing | Salt-spray testing of coated panels on request, with the result stated against the test duration |
| Masking | Threads, grounding points, sealing faces and conductive areas masked before coating |
| Other finishes | Anodising, zinc plating, brushed and satin finishing, and screen printing of logos or legends |
The parameters above are representative of typical work in this category. Your drawing defines the final specification, and every quotation states the scope it covers.
What We Do in This Area
Every job is customised to your drawing. Use these categories as a starting point for your enquiry.
Outdoor and Weatherproof Equipment
Coating systems selected for UV exposure, moisture and temperature cycling on outdoor cabinets and enclosures.
| Typical film | 60-100 microns |
| Environment | Outdoor, coastal on request |
| Key control | Pre-treatment and cure |
Indoor Cabinets and Panels
Consistent colour and finish across a batch so panels from different runs still match.
| Colour | Any RAL |
| Finish | Matte, satin, texture |
| Key control | Batch consistency |
Special Finishes and Masking
Anodising, plating, brushing and screen-printed legends, with masking on threads and grounding points.
| Anodising | Available |
| Plating | Zinc, on request |
| Printing | Logo and legends |
Capability, Tolerances & Documentation
Coating capability
| Powder | Full RAL range |
| Film thickness | 60-100 microns |
| Cure | Controlled per system |
| Effects | Matte, satin, texture |
Pre-treatment
| Degrease | Standard |
| Phosphate | Per substrate |
| Passivation | Ferrous parts |
| Rinse | Multi-stage |
Masking and detail
| Threads | Masked |
| Grounding | Masked |
| Sealing faces | Masked |
| Edges | Dressed before coating |
Where This Fits in the Production Route
Finishing starts at the cut and the weld, not at the spray booth. Sharp edges and laser dross are removed first, because a coating cannot cover a defect it sits on. Parts are degreased and pre-treated according to substrate, masked at threads and grounding points, then coated and cured to a controlled film thickness. Colour and coverage are checked against a reference panel at the start of the run, and where a batch has to match an existing installation, the exact RAL code is confirmed with you before coating begins.
- Drawing review with DFM feedback before production release
- Fiber laser cutting of the complete flat pattern in one set-up
- CNC press-brake forming, welding and grinding
- Coating applied before gaskets, hardware and glass are fitted
- First-article and sample inspection recorded for each batch
Common Questions
Yes, we coat across the RAL range. Send the RAL code, or a physical sample if the match is critical, and we confirm it before the run.
Yes, when the pre-treatment and film thickness match the environment. For outdoor cabinets we dress edges before coating, use a suitable system and can arrange salt-spray testing on request.
Yes. Threads, grounding studs, sealing faces and conductive areas are masked so they stay functional after coating.
Typically 60-100 microns depending on the specification and the environment. For a harsh outdoor or coastal application the system and thickness are confirmed at quotation stage.
Welding happens before coating. Welding a coated part damages the finish at the joint, so joints are completed and dressed first, then the part is coated.
Yes — anodising, zinc plating, brushed and satin finishing, and screen printing for logos, legends and warning markings.
Send Us Your Drawing
Tell us what you need made, the environment it works in and the quantity — we will return engineering feedback and a quotation, typically within 24 hours on working days.